Choosing a Shrink Packing Machine is not simply a matter of comparing prices or advertised speeds. The right system must match your product dimensions, film type, production volume, and available floor space. A small bakery may need an L-sealer and tunnel for boxed goods, while a beverage plant may require continuous side sealing and automatic film feeding. The decision becomes practical at the sealing jaw.
Industry data supports careful evaluation. PMMI’s 2024 State of the Industry report identifies labor availability, automation, and operational efficiency as major packaging investment concerns. These factors directly affect machine selection, especially when businesses calculate staffing, changeover time, maintenance, and energy use. Smithers’ The Future of Sustainable Packaging to 2029 also highlights increasing pressure to reduce material waste and improve packaging efficiency. A machine that runs quickly but produces wrinkled film is not efficient.
Small details matter.
Before purchasing, experienced packaging teams should test real products with the intended film. They should record seal strength, shrink uniformity, package appearance, line speed, and film consumption. A trial with frozen food, sharp corners, or uneven cartons can reveal problems that a showroom demonstration hides. Independent testing remains essential.
A reliable comparison should also examine controls, safety features, spare-parts access, operator training, and technical support. Total cost of ownership matters more than the initial quotation. The cheapest machine may create expensive downtime. Conversely, the most automated model may be unnecessary for seasonal production. There is no universal answer. This guide explains the technical and commercial factors that help buyers choose a suitable Shrink Packing Machine with greater confidence, while recognizing that every facility has limitations worth questioning.
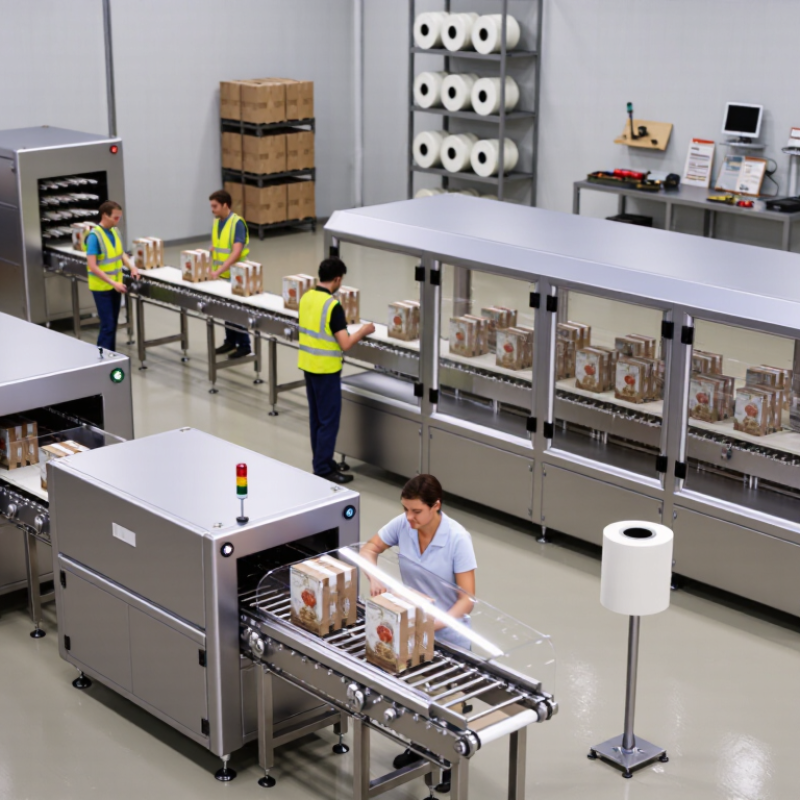
Before choosing a shrink packing machine, define exactly what will be wrapped. A glass jar, frozen tray, and printed carton behave differently under heat. Record product length, width, height, weight, surface shape, and temperature sensitivity. Measure the largest variation, not only the average unit. Small changes matter. A protruding handle may tear film or block sealing. Note whether products arrive loose, grouped, or on a conveyor. This operating detail often changes the required machine layout.
Then specify the packaging result. Do you need a tight retail finish, a dust barrier, tamper evidence, or simple bundle stability? Choose film type and thickness after checking sharp edges, moisture, storage temperature, and transport distance. Polyolefin film can suit many display packs, while thicker polyethylene may support heavier loads. These are starting points, not automatic answers. Ask for sample trials using your actual product and film. Watch the seal line, shrinking wrinkles, corner coverage, and cooling time. Record rejected packs per hour. A clean sample can hide poor consistency.
Production data should be equally specific. Estimate packs per minute, daily running hours, operator skill, available floor space, and electrical capacity. Include changeover time for different sizes. A machine matching peak speed may waste energy during normal shifts. I have seen teams overlook film storage and maintenance access. That mistake creates avoidable downtime. Request test results, safety documentation, spare-part availability, and training details from qualified suppliers. Leave room for uncertainty. Product dimensions may change after seasonal redesigns, so adjustable guides and temperature controls can protect the investment.
How to Choose a Shrink Packing Machine?
Choosing between shrink packing machine types starts with product shape, output, and film behavior. A chamber machine suits small batches, mixed products, and frequent size changes. Its enclosed sealing area reduces operator exposure to heat. Continuous side-seal machines fit stable production lines and irregular products. L-bar systems cost less, but they may create uneven corners on wide packages. Experience matters here.
Sealing method changes both appearance and maintenance. Impulse sealing works well with common polyethylene and polyolefin films. It uses brief electrical heating and usually limits energy waste. Constant-heat sealing handles thicker films more consistently, but it can increase heat exposure and residue buildup. Hot-knife sealing creates a clean side seam for high-speed lines. It needs precise temperature control. Too much heat wrinkles film; too little heat opens the seam.
The numbers deserve attention. PMMI’s 2024 State of the Industry report valued U.S. packaging machinery shipments at roughly 10 billion dollars in 2023, showing strong investment in automation. Smithers also identifies material efficiency and recyclable film compatibility as major packaging priorities through 2028. Ask suppliers for actual test samples, not only speed claims. Measure sealing strength, film consumption, warm-up time, and rejected packs. A machine rated for 40 packs per minute may deliver less with damp products or unstable film. That gap is easy to miss. Examine it before purchase.
| Machine Type | Primary Sealing Method | Typical Film | Typical Throughput | Suitable Product Size | Main Advantages | Main Limitations |
|---|---|---|---|---|---|---|
| Manual L-Bar Sealer with Shrink Tunnel | Impulse sealing on two connected film edges | Polyolefin or PVC center-fold film | Approximately 3–8 packs/minute | Small to medium products; dimensions depend on the sealing bar and tunnel opening | Low purchase cost, simple operation, flexible for short production runs | Requires manual product loading; output depends strongly on operator speed |
| Semi-Automatic L-Bar Sealer with Shrink Tunnel | Impulse sealing with powered film and product handling | Polyolefin, PVC, or compatible polyethylene film | Approximately 8–20 packs/minute | Small to medium uniform products or product bundles | Better consistency and productivity than manual operation; moderate investment | Still needs an operator for loading and film positioning |
| Automatic Side-Seal Wrapper with Shrink Tunnel | Continuous heated knife or hot-wire side sealing | Polyethylene, polyolefin, or other compatible center-fold or single-web film | Approximately 20–60 packs/minute | Regularly shaped products with consistent dimensions | High output, continuous operation, and consistent side seals | Higher cost; irregular products may require additional guides or adjustments |
| Sleeve Wrapper | Heated knife or hot-wire sealing at the film overlap or end seal | Polyethylene or polyolefin sleeve film | Approximately 10–30 packs/minute | Bundles, cartons, trays, and grouped products | Useful for multipacks; can leave product ends partially open for ventilation or access | Provides less complete enclosure than a fully sealed pouch or L-bar wrap |
| Chamber Vacuum Shrink Machine | Impulse sealing after air removal; shrink step usually uses hot water or a separate shrink chamber | Shrinkable barrier bags or vacuum shrink bags | Approximately 1–8 cycles/minute | Food, liquid-containing, or oxygen-sensitive products that fit inside the chamber | Removes air, reduces package volume, and can improve product protection | Slower than continuous wrappers; product must tolerate vacuum and sealing conditions |
| Shrink Tunnel Used with Any Upstream Sealer | Hot-air circulation or infrared heating; it does not create the package seal | Film selected according to the upstream sealing machine | Usually matched to the upstream wrapper speed | Products already enclosed in a sealed or partially sealed film package | Improves film conformity and appearance after sealing | Incorrect temperature, airflow, or conveyor speed can cause wrinkles, holes, or product damage |
| Sealing Method | How It Works | Best-Fit Films | Key Benefits | Important Considerations |
|---|---|---|---|---|
| Impulse Sealing | Electrical current heats the sealing wire for a short, controlled cycle while pressure is applied. | Polyolefin, PVC, polyethylene, and many multilayer films, subject to film specifications | Low energy use while idle, adjustable sealing time, and suitability for intermittent operation | Seal quality depends on temperature, dwell time, pressure, and clean film surfaces |
| Constant-Heat Sealing | Heated sealing jaws or bars remain at a controlled temperature during operation. | Polyethylene, laminated films, coated films, and heat-sealable webs | Suitable for thicker films and continuous production | Requires careful temperature control to prevent weak seals, film distortion, or sticking |
| Heated Knife or Hot-Wire Sealing | A heated blade or wire cuts and seals the film in one operation. | Polyolefin, polyethylene, PVC, and other compatible shrink films | Fast continuous side sealing and clean separation of film webs | Film thickness, speed, and knife temperature must be matched to avoid incomplete seals or smoke |
| Vacuum Impulse Sealing | Air is removed from the bag before an impulse bar creates the final hermetic seal. | Vacuum pouches and shrinkable barrier bags with a compatible sealant layer | Reduced oxygen and package volume; useful for products requiring close-fitting protection | Not suitable for every product; sharp edges, liquids, and excessive vacuum may affect package integrity |
Note: Throughput figures are typical planning ranges rather than guaranteed outputs. Actual performance depends on product dimensions, film type and thickness, operator loading, sealing time, tunnel temperature, and conveyor speed.
Machine capacity should match your real production rhythm, not an optimistic sales forecast. Measure products per minute, pack dimensions, changeover frequency, and peak-season demand. A 40-pack-per-minute machine may underperform when operators handle irregular cartons. The global shrink packaging market was valued at approximately USD 11.7 billion in 2023, according to Fortune Business Insights. This growth increases pressure to select equipment that can scale without creating bottlenecks.
Speed is useful only when sealing, shrinking, and cooling remain stable. Ask for tested output using your actual product and film. PMMI reports that labor shortages continue pushing packaging companies toward automation and easier machine operation. Still, faster equipment can produce more wrinkles, weak seals, or film waste when settings are poorly matched. That part is often underestimated. Review seal temperature, conveyor speed, tunnel airflow, and recovery time between product changes. A machine rated at 60 packs per minute may deliver less in daily production.
Film compatibility deserves equal attention.
Polyolefin, polyethylene, and PVC films require different sealing temperatures, shrink ratios, and tunnel conditions. Confirm film width, thickness, centerfold format, and maximum shrink percentage before purchasing. ASTM D882 testing data can help compare film tensile properties, while supplier trials reveal practical behavior.
Do not rely on a sample roll alone. Test printed film, cold products, sharp corners, and uneven loads. A machine that performs well in a showroom may struggle beside a dusty production line. Record rejected packs and film consumption during a full shift; the results may challenge your original choice.
Automation should match your operators, products, and production rhythm. Look for recipe storage, automatic film tracking, temperature control, and clear fault messages. These features reduce repeated adjustments during changeovers. The International Federation of Robotics reported 541,302 industrial robots were installed worldwide in 2023. That figure shows broader automation growth, but more automation is not always better. A small operation may need reliable semi-automatic controls instead of a complex system.
Space is unforgiving. Measure the machine, loading area, film storage, electrical points, and maintenance clearance. Leave enough room to open panels without blocking walkways. Check ventilation requirements around heat-sealing components. PMMI’s 2023 State of the Industry report valued U.S. packaging machinery shipments at about $10.2 billion in 2022, reflecting strong investment across varied facility sizes. Still, a machine that fits on paper may disrupt material flow in practice. Mark its footprint with tape first.
Safety and maintenance deserve equal attention. Select guarded heat zones, accessible emergency stops, interlocks, and documented risk controls. Confirm that the design supports applicable workplace safety requirements. Ask how quickly technicians can clean the sealing bar and replace wear parts. A useful interface should show alarms, temperature trends, and service reminders. Shorter maintenance access can protect uptime. Sometimes, it does not. Request realistic demonstrations using your film and product sizes, because catalog performance rarely reflects every production condition.
Choosing a shrink packing machine requires more than comparing purchase prices. Total cost often decides whether the investment remains practical.
Calculate film consumption, electricity, compressed air, labor, maintenance, and expected downtime. A lower-priced machine may waste more film or require frequent adjustments. Measure your current production data instead of relying on sales estimates. For example, a small sealing delay repeated every cycle can reduce daily output noticeably. I once underestimated spare-part costs on a packaging project, and the operating budget changed within months. That mistake was avoidable.
Supplier support should be assessed as carefully as machine performance. Ask about response times, technician availability, training, and spare-part storage. Request clear maintenance schedules and written troubleshooting procedures. Practical support matters during a late-night stoppage. Promises are easy. Verify them through customer references and factory acceptance testing.
Think about future expansion before signing the order. Check whether the machine can handle wider film, higher speeds, or additional product sizes. Confirm compatibility with conveyors, printers, inspection devices, and existing control systems. Leave enough floor space for another unit or a larger film roll station. Utility capacity also matters, especially for compressed air and electrical loads. Test your actual products and films before purchase. A machine may perform well in a demonstration but behave differently on a dusty shop floor. Growth is rarely tidy, so flexible design can protect the next investment.
Five-Year Total Cost Comparison: Purchase, Support, Labor, and Expansion
This planning model compares typical five-year ownership costs for three machine configurations under a two-shift production schedule. The estimates include equipment purchase, installation and training, maintenance and spare parts, labor, and future expansion. Although automatic systems require more capital initially, their lower labor cost and stronger expansion potential can reduce total cost over time. Actual results depend on production volume, local wages, film consumption, machine uptime, and supplier service coverage.